LED Control Plan: What OEM Buyers Should Require From Production Quality Control
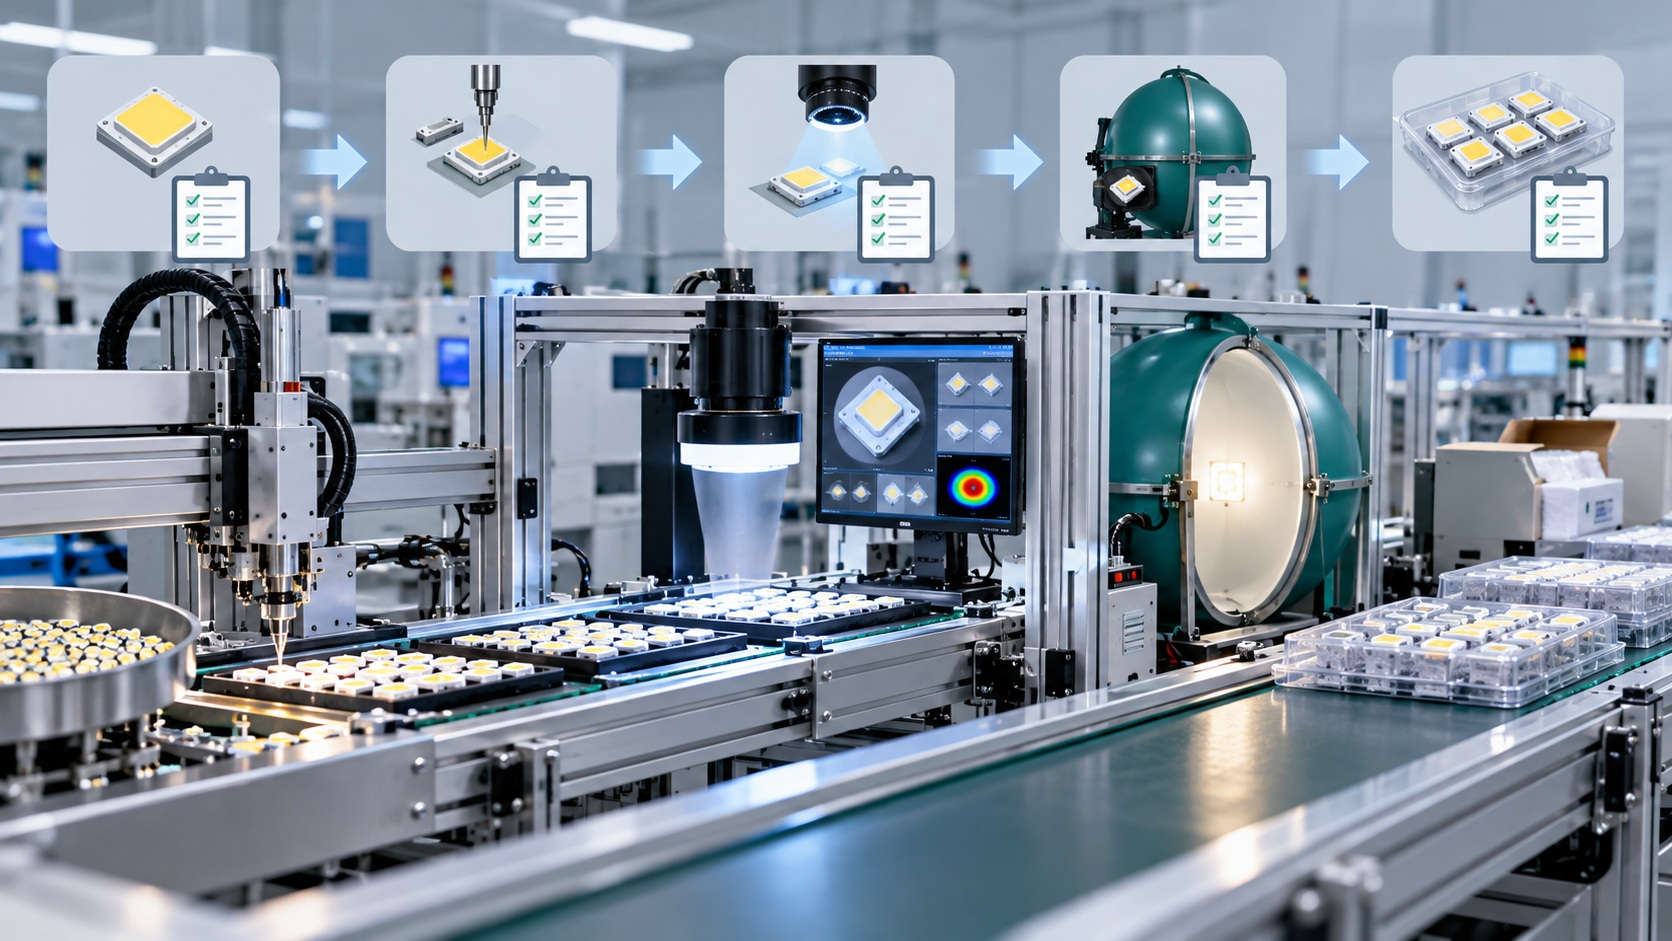
Quick Answer: What an LED Control Plan Controls
An LED control plan names every production step that can affect the delivered part and pairs it with a control. The control is normally a measurement, an inspection or a machine parameter, and each one carries a frequency, a limit and a named owner.
The plan is also a reaction document. For every control it should state what happens when a result moves outside the limit, so the response does not depend on which operator is on shift.
That pairing of control and reaction is why buyers ask for the plan rather than only the process flow. It is the shortest way to see how variation is actually managed on the line, and it is the document an auditor will test against records.
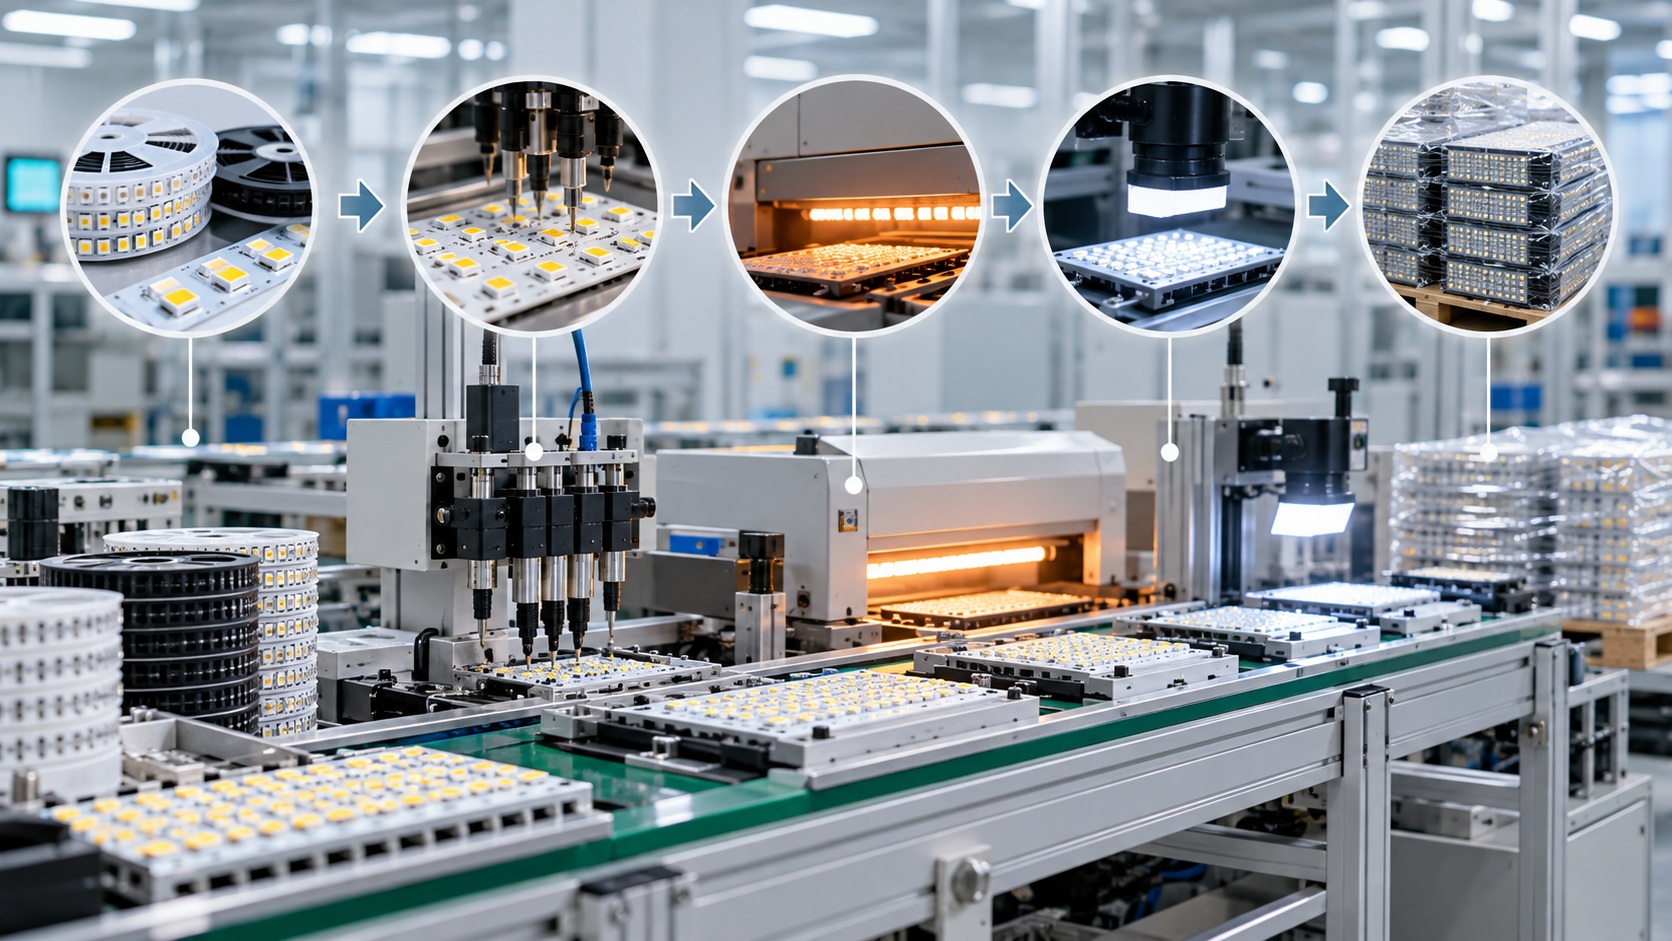
Which Production Steps Belong in the Plan
The steps that matter most are the ones that cannot be inspected back into specification afterwards. Die attach, wire bonding, encapsulation and reflow conditions all belong to that group, because a defect introduced at those steps stays hidden until reliability testing or field use exposes it.
Incoming material, pre-assembly checks and final testing also belong, but they sit at a different risk level and are usually owned by a different team. The plan should make that ownership explicit rather than leaving two departments to assume the other is checking.
For a buyer, the practical reading test is simple. Read the plan beside the process flow and look for any step that appears in one document but not the other. A missing row on either side is usually where an unverified characteristic is passing through unnoticed.
Evidence and Documents to Request
Request the plan as a controlled document with a revision number, not as an unprotected spreadsheet attachment. Beside it, ask for the instrument list with calibration intervals, because a limit only means something if the instrument that reads it is in calibration on the day of production.
The rest of the evidence set overlaps with a supplier assessment, and our LED supplier audit checklist sets out the document groups a buyer normally reviews before a visit. The control plan is one of those process-control documents rather than a separate exercise with its own logic.
Where the plan is used to release material rather than to build it, the checks performed on receipt are described in our guide to incoming inspection for LED components. The two documents should agree on which characteristic is verified at which site, otherwise the same parameter is either checked twice or not at all.
Acceptance Criteria: What Makes a Control Plan Acceptable
Acceptance should be decided row by row rather than as a single yes or no. A plan with strong controls on bonding but a vague reaction rule still leaves the buyer exposed at the one step where it matters most.
| Production step | Control to expect | Record | Reaction rule |
|---|---|---|---|
| Incoming material | Certificate review plus sample check against the specification | Receiving record with lot reference | Lot held and supplier notified before release |
| Die attach | Machine parameter log and periodic shear or visual check | Parameter log with check interval | Line stopped, affected units quarantined and traced |
| Wire bond | Pull or visual inspection at a defined frequency | Inspection record with sample size | Rejection triggers re-inspection of the interval since the last good check |
| Encapsulation | Process parameters and cured-state inspection | Parameter and inspection record | Batch held for rework or scrap decision |
| Reflow or assembly | Profile verification against the approved profile | Profile chart with date and line | Profile corrected and affected boards identified |
| Final test | Optical and electrical measurement against the specification | Test result file linked to the lot | Failures confined to a lot boundary and dispositioned |
Two of those columns carry most of the buyer value. The record column shows whether the control leaves evidence, and the reaction rule column shows whether the supplier has thought about failure rather than only about pass and fail.
Strong LED supplier quality practice is visible in the reaction column. A supplier that can describe containment and traceability without hesitating is describing a process it has already had to use.
Change, Exception and Deviation Handling
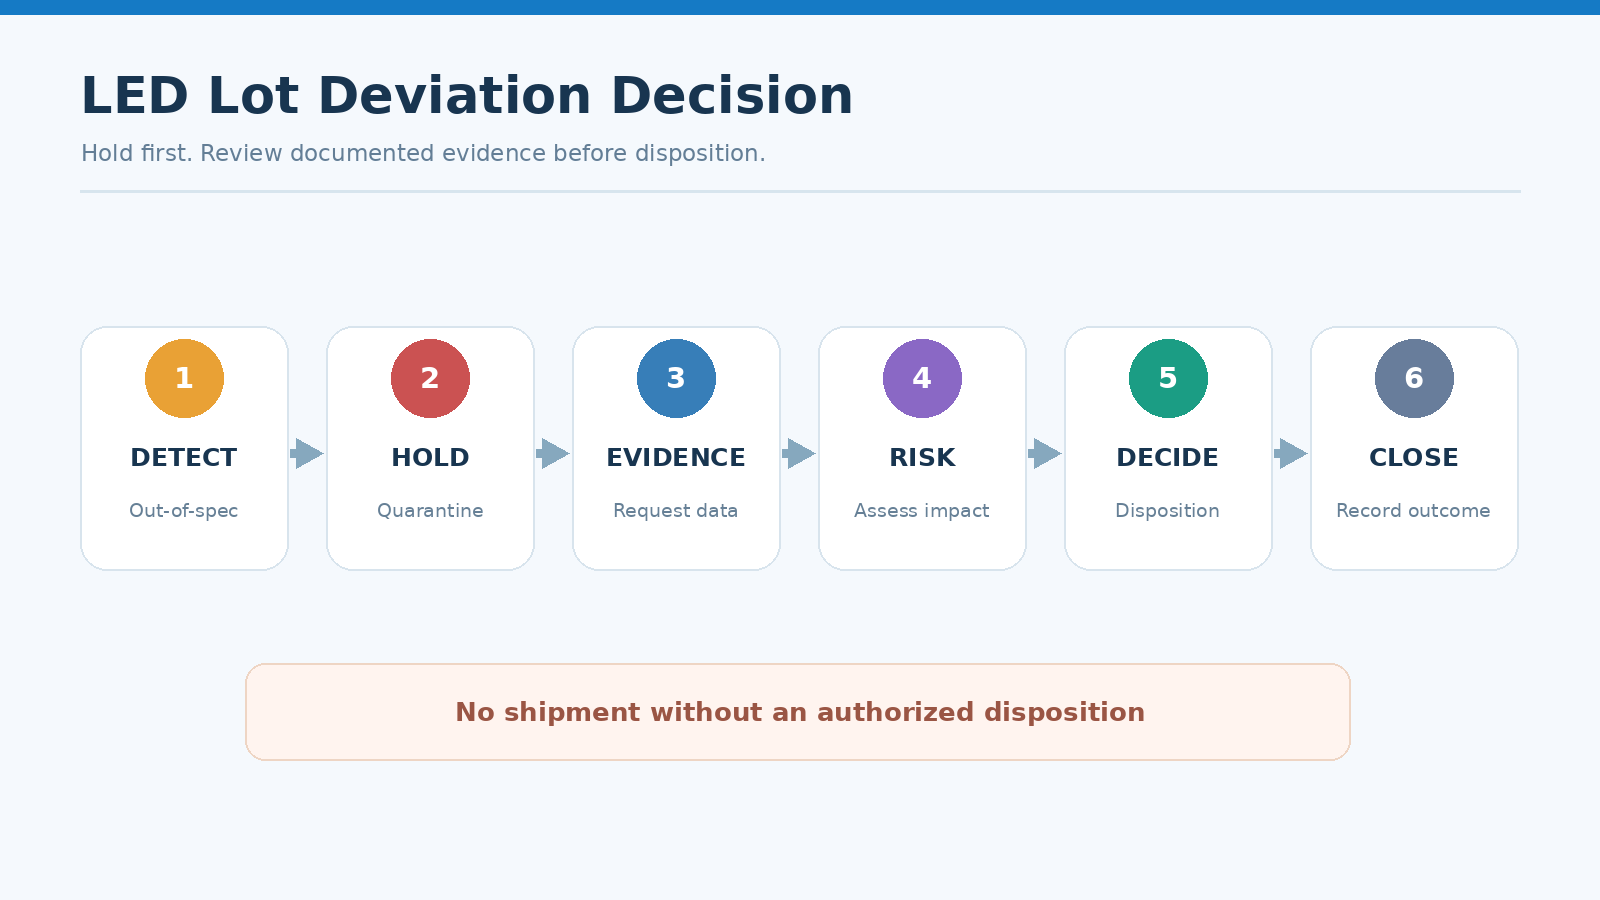
A plan that cannot describe its own exceptions will be bypassed in the first difficult week of production. Each exception should have a defined route: who may approve it, how long it stays open, and what evidence closes it.
When a failure reaches a later stage or the field, the corrective loop should be traceable back to the plan. Our article on LED 8D corrective action explains how prevention updates such as a revised control plan are recorded, and that revision step is where the document becomes a living record instead of a one-time attachment.
The commercial counterpart is the production approval package. An LED PPAP submission uses control-plan evidence as one of its elements, so a supplier that maintains the plan continuously can assemble that package without reconstructing evidence after the fact.
This is the area where Supplier Change & Quality Management earns its place in a procurement file. Changes are not only announced by a notification letter. They often appear first as a quiet edit inside a production document, and a revision-controlled plan makes that edit visible.
Buyer Checklist and RFQ Handoff
Before the requirement leaves the desk, the buyer should be able to state which characteristics are controlled by the supplier, which are verified on receipt, and which are fully specified by the drawing. Anything that remains unassigned is a gap that will surface at the least convenient time.
Writing that division into the inquiry stage avoids negotiating it later. OEM LED procurement teams that include it consistently report fewer open questions during the first production build, because the responsibility boundary was agreed while it was still cheap to change.
Keep the checklist short enough to re-run at every revision. Three questions are enough to test a resubmitted plan: what changed, which control proves the change, and which record will show that the control ran.
Frequently Asked Questions
What should OEM buyers require for LED control plan review?
A buyer should require a revision-controlled plan that names each production step together with its control, frequency, record and reaction rule. The measurement instrument list with calibration intervals should accompany it so the limits can be judged.
Which documents or evidence matter for LED control plan approval?
The plan itself, the process flow it maps onto, the instrument and calibration list, and representative records from a recent production run form the core evidence. A change note per revision completes the set that makes the plan auditable.
How should a supplier and buyer define acceptance for LED control plan content?
Acceptance should be defined row by row, with the control and the reaction rule agreed for each step that can affect the delivered part. Rows that cannot be verified at the supplier should be reassigned to receiving inspection or to the drawing.
What should be checked before approving LED control plan revisions?
Confirm which rows changed, why they changed and what triggered the revision before approving anything. Then verify that the new control is running and that a record exists for the first production lot built under it.
Does a control plan replace the process flow or the inspection standard?
No, it sits between them and references both. The flow defines the route, the inspection standard defines how a characteristic is measured, and the control plan decides where and how often each of those checks is applied.
Conclusion: Read the Plan, Not the Brochure
An LED control plan is the document that shows whether a supplier manages variation deliberately or absorbs it quietly. A buyer who reviews it row by row learns more about production quality control than any capability brochure can convey.
Start with the steps that cannot be inspected back into specification, confirm a record exists for each control, and insist that every control carries a reaction rule. If you are preparing an OEM requirement and want the control-plan and evidence set reviewed against your project, send your project requirements to the HOUKEM team and we will confirm the applicable documentation scope.
COA vs COC LED Components: Which Certificate Fits a Shipment
LED Supplier Deviation Approval for Components: When to Accept and When to Reject